Custom Metal Stamping Parts
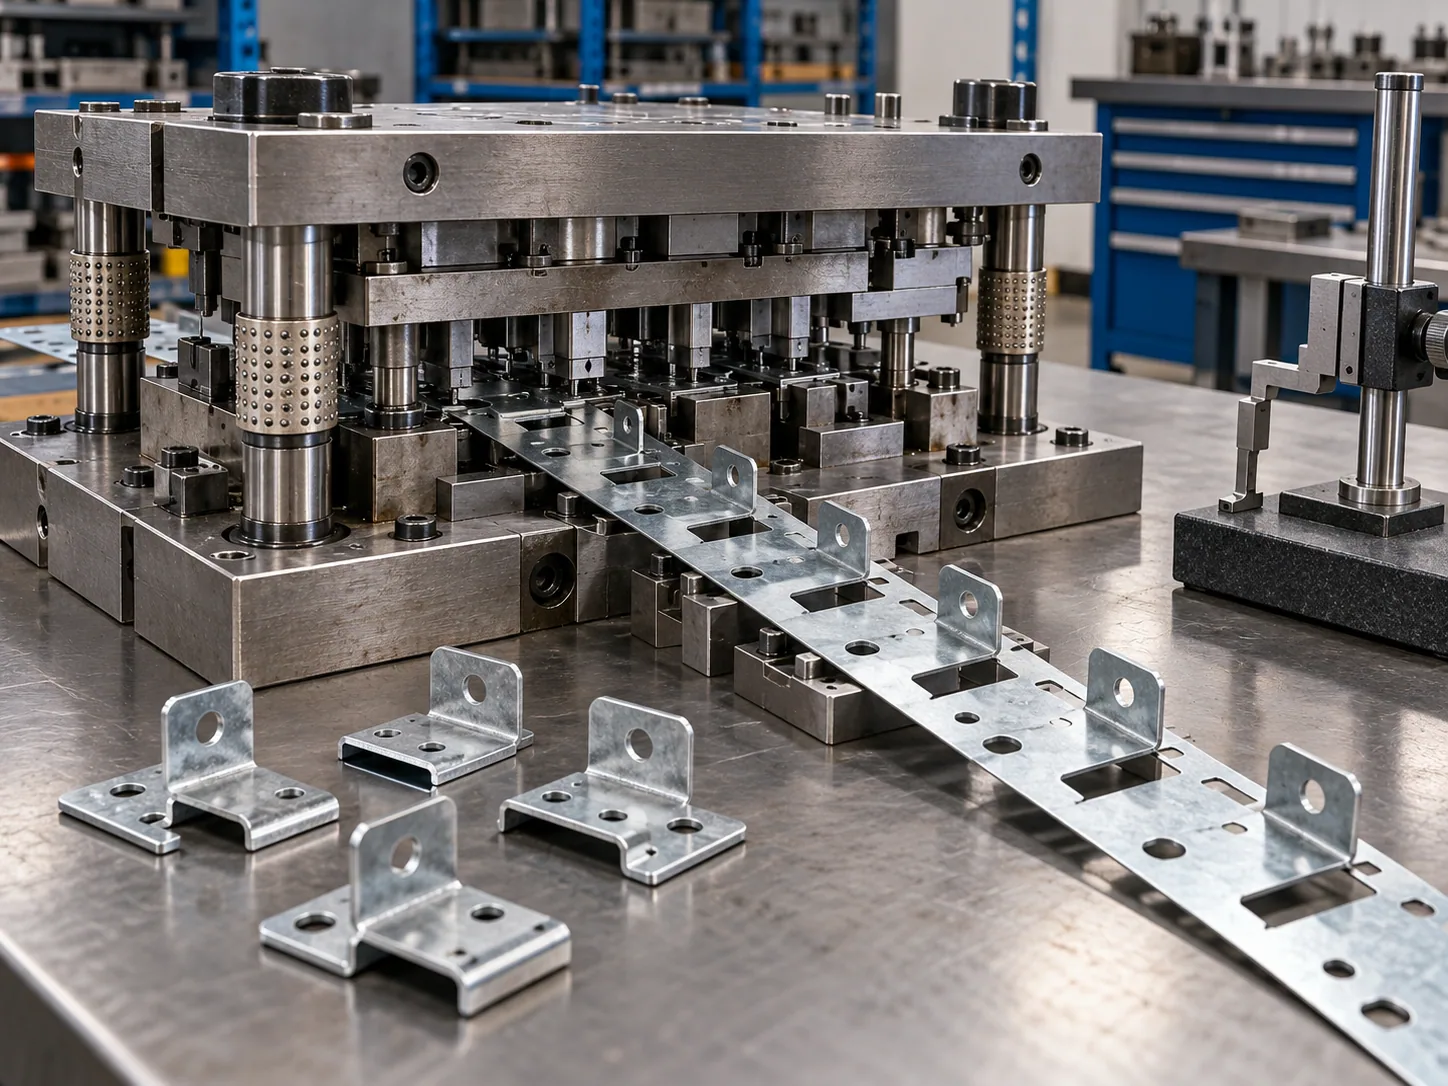
Harmonyos Metal Stamping manufactures custom stamped parts to customer drawings — brackets, clips, mounting plates, retainers, terminals and formed components in carbon steel, stainless steel, copper and aluminum. Presses run from 30T to 400T, thickness from 0.5 mm to 10 mm, and parts ship to OEM and Tier-1 buyers across Southeast Asia.
This page covers what we make and how to specify it. If you already know your process, the metal stamping capabilities page goes deeper into press selection and die design.
Parts we manufacture
| Part family | Typical use | Page |
|---|---|---|
| Steel brackets | Structural supports, frame connections, panel mounting | Steel brackets |
| L brackets | Corner joints, shelf supports, enclosure corners | Custom L brackets |
| U brackets | Shaft supports, channel mounts, cable guides | U brackets |
| Mounting plates | Motor mounts, sensor plates, base plates | Mounting plates |
| Stamped clips | Retaining, spring and grounding clips | Stamped clips |
| Zinc-plated brackets | Outdoor and humid-environment brackets | Zinc-plated brackets |
If your part does not fit a family above, that is normal. Most of what we run is a one-off geometry with its own die.
Specification summary
| Material | Q235 carbon steel, SPCC cold-rolled steel, 304 stainless steel, copper, aluminum, customer-specified grades |
|---|---|
| Thickness | 0.5–10 mm, confirmed per drawing and application |
| Press range | 30–400 T |
| Processes | Blanking, piercing, bending, forming, deep drawing |
| Finish | Zinc plating, powder coating, electrophoresis, deburring |
| Sampling | Small-batch samples in 7 days after requirements are confirmed |
| Production | 15–25 days after sample approval |
| Monthly capacity | Approximately 100 tons, subject to product mix |
| Inspection | Height gauges, inspection fixtures, CMM; reports on request |
| Quality system | ISO 9001, established 2011 |
Choosing material and finish together
Material and finish are usually specified separately on a drawing, but they interact. A few patterns come up often:
- Indoor brackets, painted assembly. SPCC with powder coating. Cold-rolled sheet forms cleanly, and the coating hides minor handling marks.
- Outdoor or humid service. Q235 or SPCC with zinc plating, or 304 stainless if the part also sees salt or washdown. Zinc thickness matters more than the label — confirm it on the drawing.
- Visible parts on consumer equipment. 304 stainless, brushed or with a powder coat matched to the housing. Forming marks show on stainless more than on painted steel.
- Electrical and conductive parts. Copper or aluminum, with plating chosen for contact resistance rather than appearance.
- Complex geometry, hidden surfaces. Electrophoresis reaches inside formed sections that spray coating misses.
Detail on each option is on the materials and surface finishing page. If two specifications would both work, send both — we will tell you which is easier to form and which has the shorter lead time.
What drives the price
Four things, in roughly this order of impact:
- Tooling. A single-stage die for a simple bracket is a modest one-time cost. A progressive die for a multi-feature part is a real investment and only pays back at volume. Tell us the annual quantity, not just the first order.
- Material utilization. The gap between parts on the strip is money. A small geometry change — a shorter tab, a tighter corner — can move utilization by several percent, which compounds across a production run.
- Number of operations. Every additional bend or pierce adds a station, a handling step and a chance for variation. Parts designed for one hit are cheaper than parts assembled from three stampings.
- Finish and inspection. Plating and coating are priced by surface area and process. CMM reports and first-article documentation add cost, but they are usually cheaper than a rejected shipment.
We quote against your drawing rather than a catalogue price, because none of the above is knowable from a part name.
Quality and documentation
Sampling includes dimensional inspection against the drawing. Production runs start with a first-article check, and in-process inspection continues at an agreed frequency. Height gauges handle routine dimensions; dedicated fixtures hold critical ones; the CMM covers geometry that cannot be checked by hand.
Inspection reports are available on request, and we agree inspection points during drawing review for parts with a critical fit. See quality control for how that is set up.
Frequently asked questions
Can you produce from a 3D model only?
A STEP file is a good start, but stamping needs a flat pattern, material, thickness and tolerance callouts. Send the model and we will tell you what to add. Sheet metal parts modelled without bend allowance often need adjustment before the die is cut.
Do you make small quantities?
Yes, and small-batch samples are how most projects start. The economics change with the die: a simple bracket supports low volumes, a progressive-die part does not. MOQ is confirmed per part in the quotation.
Can you match an existing part from another supplier?
Yes. Send the part or a drawing. If you send a physical sample, expect us to measure it and produce a drawing for confirmation — a worn part does not define the nominal.
How do you handle tolerance questions?
We confirm achievable tolerance per drawing during review and state it on the quotation. We do not publish a single blanket figure, because it would be wrong for most parts.
What about packaging and shipping?
Parts are packed to protect edges and finishes, with labels matching your part numbers. We support customers in Malaysia, Vietnam and Thailand, and quote other destinations on request.
Request a quote
Send your drawing, material, thickness, finish, quantity and target date to robert@hmstamping.com, or use the quote request form. The RFQ checklist lists what makes a quote accurate on the first pass.
Related: stamping capabilities · bending · deep drawing · industries we serve
Temporary Harmonyos metal stamping product photo"harmonyos-ai-grid">
KEEP READING